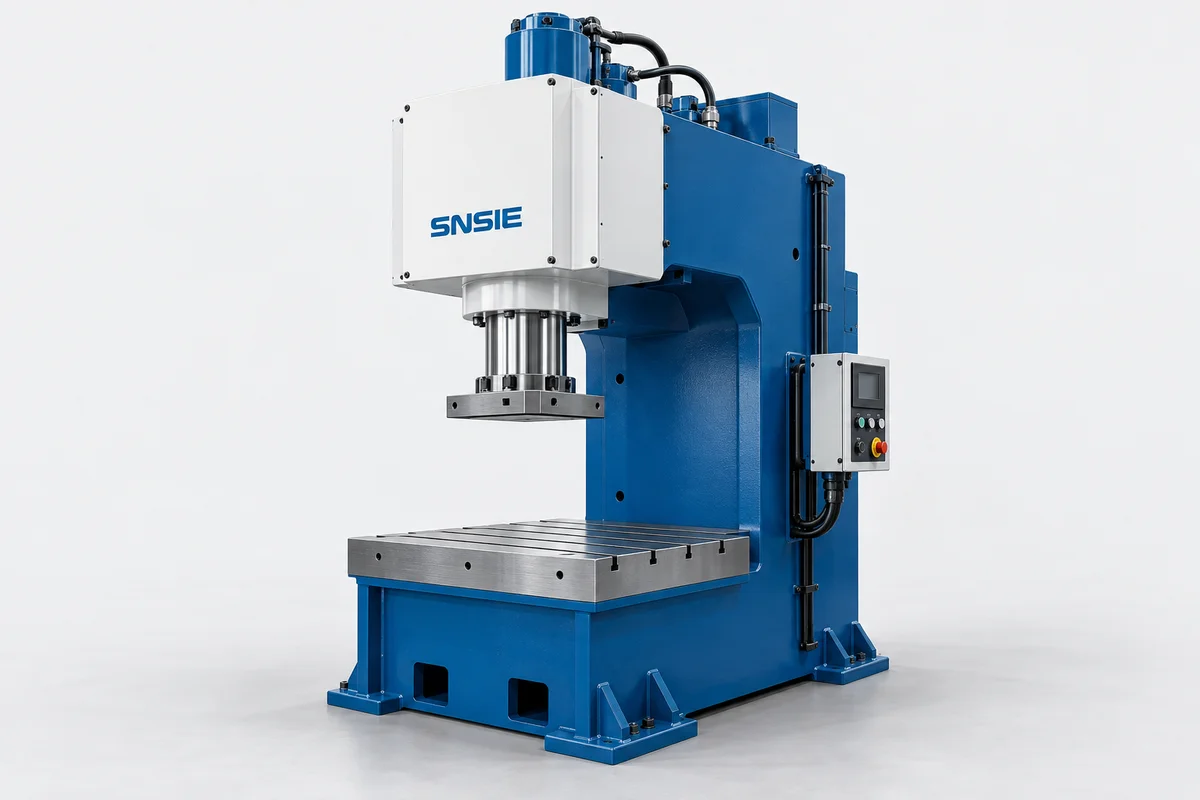
Hydraulic C-frame press
Open-front hydraulic pressing with pressure and stroke set for the process.
- Hydraulic force application
- Open-front tooling access
- Pressure/stroke adjustment
Hydraulic C-frame and pneumatic-clutch power presses for punching, pressing and die forming.
Presses apply force through a die to punch, form or assemble parts. Hydraulic and crank-driven systems differ in force, energy and stroke characteristics.
Open-front hydraulic pressing with pressure and stroke set for the process.
Crank-driven stamping with pneumatic clutch control for repeated die operations.
Review die drawings, force curve, shut height, stroke and off-center load. Include feeding, scrap removal, die protection and safeguarding.
Discuss your application →Metal blanks or coil stock with dies matched to material, thickness, lubrication and forming process.
Use these fields to compare a proposed machine against your material, drawings and production needs.
| Specification | What to confirm |
|---|---|
| Rating | Force curve, load position and available energy. |
| Die envelope | Bed, shut height, stroke and slide adjustment. |
| Production | Cycle rate, feeding and scrap removal. |
| Protection | Guards, die monitoring and overload control. |
Working capacities and available options depend on the selected model. Request a technical sheet for your material and part.
Request specifications →Review die drawings, force curve, shut height, stroke and off-center load. Include feeding, scrap removal, die protection and safeguarding.
Start with the required process and part drawings, then review the capacity, tooling, control and installation details of the proposed model. Include representative parts when production quality or cycle time is critical.
Share your sheet-metal processing requirements with SNSIE.